
Guide scope
Reader: product development, quality, plant engineering, and procurement teams.
Task: turn a waffle or pancake target into a documented brief, controlled trial, and commercial handoff.
Boundary: product quality observations do not prove food-safety release, cleaning performance, or equipment suitability.
Questions about how to use waffle and pancake guides tend to stop at recipes. In contrast, production teams have to outline what the end product looks like, differentiate the formula from process variables, determine the forming route, and capture what a commercial trial indicates. This guide links these decisions together without using one good sample as a validated process.
Waffle and Pancake Guides are production-planning resources for production teams: start with measurable product targets, compare how each format contacts heat, test controlled variables, and confirm the result on the proposed commercial configuration. Formula, equipment, sanitation, scale-up, and acceptance remain separate evidence questions.
Key points
- Waffle and pancake names aren’t equipment specifications.
- A peer-reviewed pilot-scale waffle experiment shows that sticking can vary by recipe; its values are specific to that study and process.
- Treat the 6-Control Product-to-Trial Map as an editorial planning worksheet, not a standard.
- Pilot results must be checked again when batch size, mixing, heating, holding, or equipment geometry changes.
- Texture acceptance and food-safety release require different owners and evidence.
Start with the finished-product brief, then test the whole process context
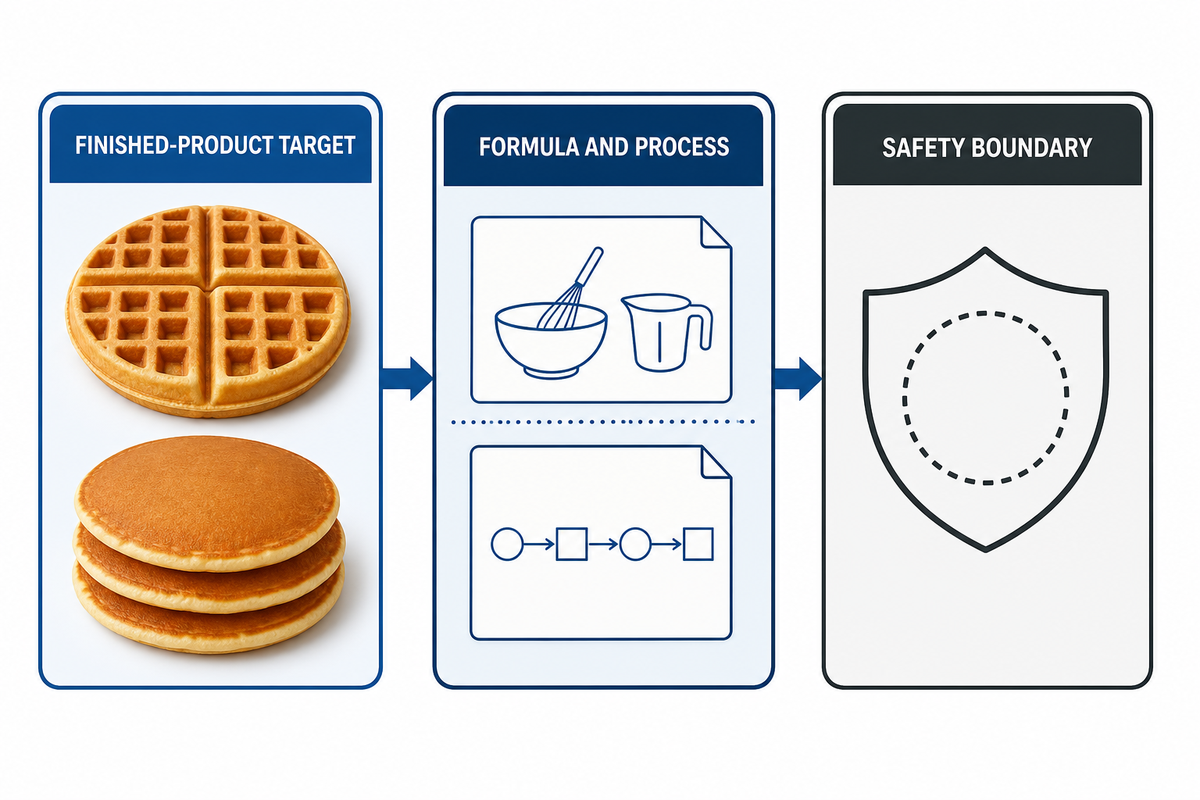
A finished-product brief should identify the waffle or pancake that needs to reach the customer, then link this to the formula, equipment, process, packaging, intended use, sanitation, and hazards. This brief initiates a commercial discussion, and isn’t intended to compensate for the facility’s hazard analysis or to select equipment on its own.
Add geometry, piece mass, surface pattern, target color, eating texture, serving temperature, topping or inclusion conditions, and the point at which texture will be evaluated. If “crispy waffle” is the desired product, and the buyer expects crispness after a 20-minute hot hold, then this description is too broad. If the buyer expects “Soft pancake” and the diameter, thickness, degree of doneness, packing method, and reheating state are undefined, then this description is also inadequate.
Since product attributes can move together, product design can be tricky without broader context. For example, formula can influence attributes such as viscosity and structure. Substrate composition and thermal history can influence final set, appearance, and release from the mold. Holding and packaging can influence the final texture delivered to the customer. Therefore the buyer should identify whether each field is defined, still unknown, or is the responsibility of a particular department such as product development, quality, food safety, engineering, or procurement.
For facilities within the U.S. that are covered, 21 CFR 117.130 includes the evaluation of hazards involving formulation, design of the facility and equipment, raw materials, processes of manufacturing and packing, packaging, labeling, storage, distribution, and the intended use and sanitation. While this section of the rule isn’t a waffle-design worksheet, it aids in differentiating a product brief from a complete safety hierarchy.
Buyers may argue that these questions will delay the quotation. This is usually the case. Without a detailed product description, the supplier can’t guarantee an acceptance trial. Use the commercial waffle and pancake production overview when the brief is finalized and ready for discussion in relation to specific equipment.
Waffle vs pancake: compare the production consequences
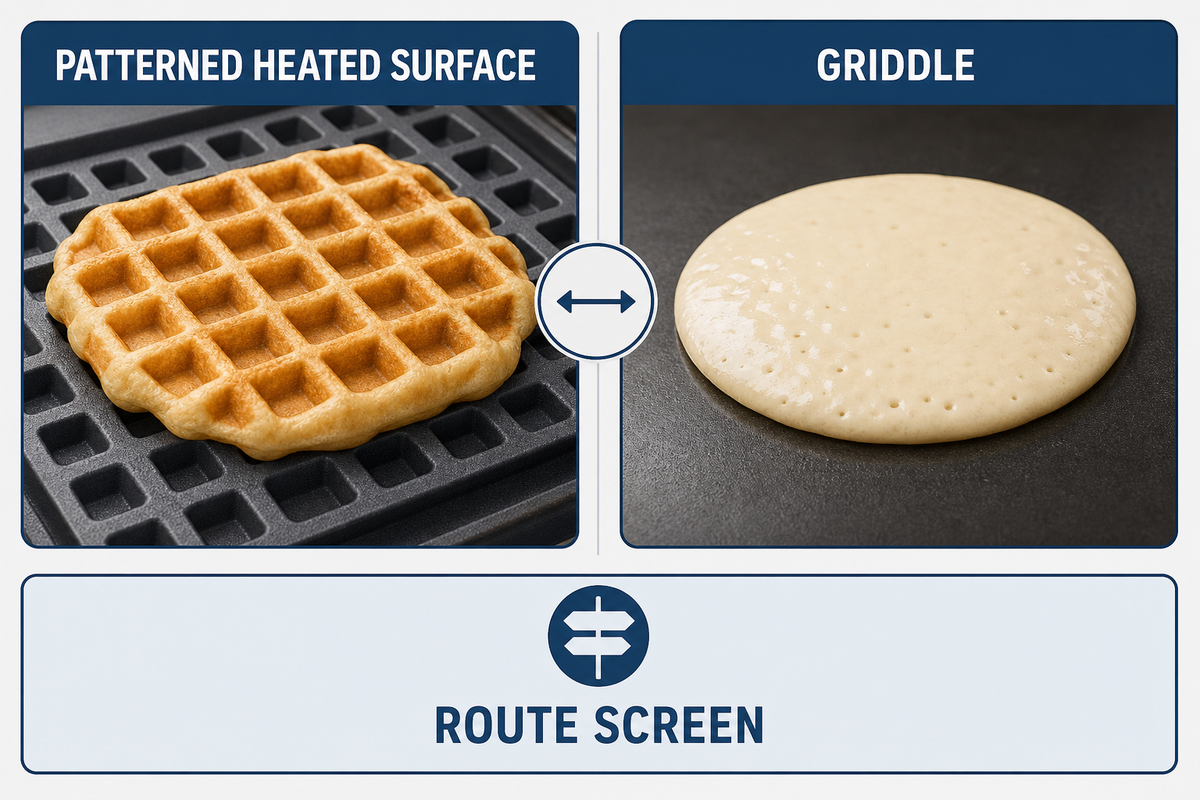
Searches for “pancakes and waffles difference” may start with ingredients from the same family; however, forming and heating processes differ because batters contact the equipment differently. A waffle presses against a patterned heated surface, while a pancake is generally prepared by spreading batter on a griddle and exposing its upper surface before turning or passing through another heating stage.
Plate-based waffle route
- Patterned cavity defines the outer geometry.
- Two-sided surface contact makes release a primary trial result.
- Plate condition, fill amount, heat history, and opening time interact.
Griddle-based pancake route
- Deposit and spread help define diameter and thickness.
- One face is initially open before turnover or later heating.
- Deposit consistency, surface recovery, turning, and transfer need proof.
A cone, thin shaped wafer, Japanese-style thick pancake, or crepe-like product can add another route. This table screens questions; it doesn’t select a current UDTECH model or promise that one line covers every format.
| Product type / cue | Production consequence | Evidence to request | Limitations / Not suitable for |
|---|---|---|---|
| Deep-grid waffle | Cavity fill and release shape the piece | Filled-cavity trial and released sample | Flat-griddle result cannot prove cavity release |
| Thin crisp waffle | Heat and post-bake handling affect fracture | Condition at release and after hold | Fresh sample does not prove packed texture |
| Belgian-style target | Label alone leaves grid, depth, and bite open | Reference sample and dimensioned drawing | No universal Belgian geometry applies |
| Standard pancake | Deposit spread and turnover affect shape | Deposit record and browning pattern | Waffle-plate proof does not transfer |
| Thick pancake | Thickness changes the heating question | Section view and product-specific trial | Thin griddle settings are insufficient |
| Continuous griddle product | Deposit must track a moving heat surface | Line-speed basis and deposit consistency | Stationary-pan behavior is not line proof |
| Waffle cone or shaped shell | Forming continues after heating | Tooling, forming window, and cooled shape | Plate-waffle release alone is insufficient |
| Crepe-like sheet | Thin spread and later folding need review | Sheet thickness and downstream handling | Thick-pancake route may be unsuitable |
| Filled or topped format | Downstream dose and moisture alter the result | Final product after the agreed hold | Plain-piece acceptance cannot release it |
What makes waffle batter different from pancake batter?
Waffle and pancake batters may begin with similar ingredients; however, a commercial formula should be based on the contact surfaces, geometry, release, color, and the texture of the service. Ingredient lists don’t prove that one batter will make both products acceptable.
The peer-reviewed pilot-scale waffle study using equipment that simulates industrial baking connects sticking and take-off with recipe ingredients, batter stability, plate material, release agent, baking conditions, cleaning, and ambient conditions. This study reports 30 waffles per recipe and sticking percentages of 6.7% versus 46.7%. This suggests that, when you take the “same mix, different appliance” shortcut, you must verify that the effects are consistent with the process window. Study values are specific to that process and don’t define a universal process window. To define the geometry of a waffle without prematurely assigning equipment, you can use this waffle style reference.
Build batter around the target eating texture
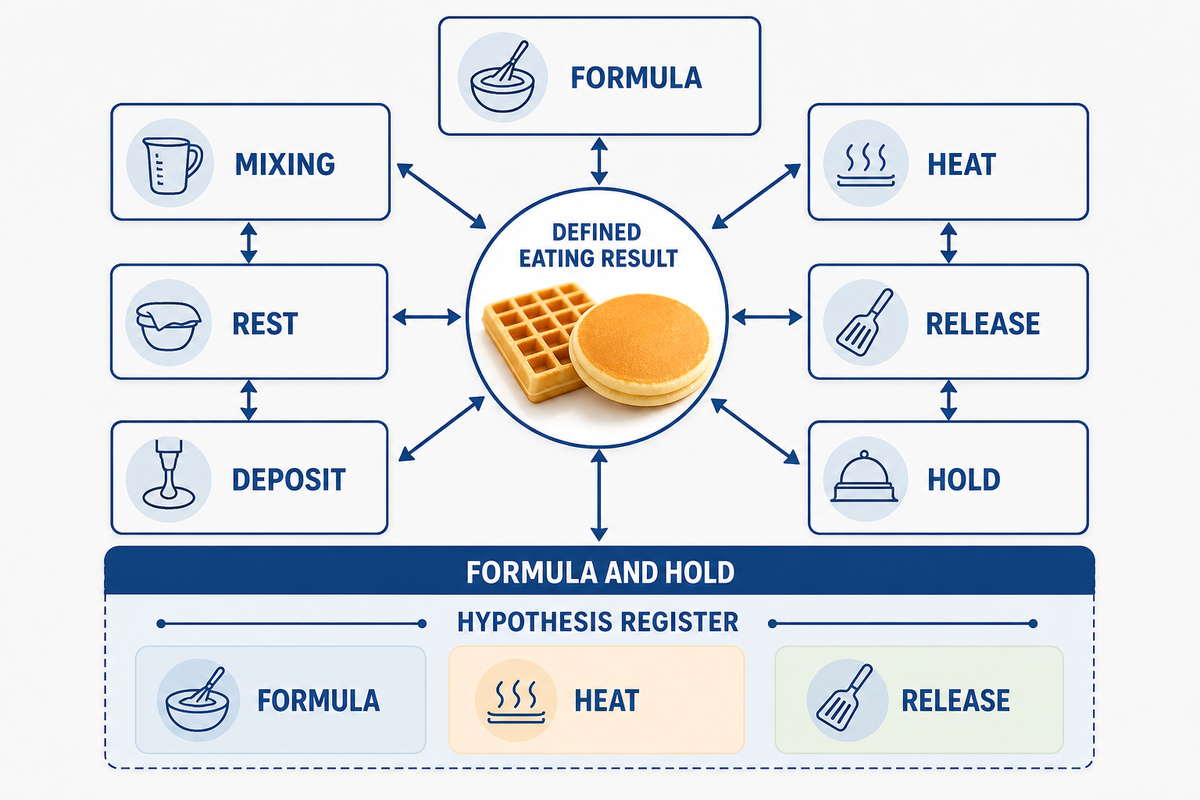
Production batter should be developed around a defined eating result and the process that produces it. Formula, mixing, rest, deposit, heat, release, and hold can interrelate and interact, so a failed waffle or pancake shouldn’t be assigned to one ingredient or one machine setting until the team has documented all competitive causes.
Start with the hypothesis register. Formula fields can include flour basis, egg system, sugar, oil or melted butter, leavening (baking powder), added water or whole milk, and any buttermilk, whole-grain, non-dairy, blueberry, or topping, etc., relevant to the product. Process fields should include mixing sequence, batter temperature, rest time, amount of batter, deposit behavior, preheat state, actual heating conditions, release method, and hold before inspection.
Consumer search language may label things concisely, but can’t define production specifications. Breakfast buyers may use labels such as buttermilk pancakes, blueberry pancakes, homemade pancakes, homemade waffles, a favorite pancake, a favorite waffle, or leftover waffles to be reheated in a toaster; searches for “best waffle and pancake guides” still require a defined reference product. Indicate if your target uses whole grain or non-dairy ingredients, maple syrup or other waffle topping, and if egg whites, whole milk, vanilla extract, canola oil, vegetable oil, melted butter, or baking powder should be part of the formula.
Recipes and popular cookbooks may say “whisk together the dry ingredients in a large mixing bowl,” “preheat your waffle maker,” “don’t overmix,” or cook in a “nonstick skillet over medium heat” with a spatula. Other directions promise the best waffles, perfect waffles, a crispy outside, or a batch of waffles that is crispier on the outside. Those phrases can identify the reference product, yet a waffle mix, pancake and waffle mix, or waffle and pancake recipes can’t define a factory window. To make waffles or pancake mix waffles, a home recipe may add melted butter or oil and let the batter sit. However, production will require a measured waffle batter or pancake batter condition, the amount of batter, a documented contact surface other than a large nonstick pan, and a different result for each different pancake or waffle target.
Treat the register as a barrier between familiar kitchen advice and an industrial standard. “Don’t overmix,” “let the batter sit,” or “add vegetable oil for a crispier outside” may be suggested ideas. These still require a defined formula, scale, method, and response. Large mixing bowls, bakery mixers, pumps, and hoppers expose batter to different shear, residence, and temperature histories.
What type of pancake mix works best for waffles?
There’s no optimal pancake mix for waffles. A candidate mix works best when it achieves the optimal cavity fill and surface definition with the desired release, color, crispness, tenderness and holding behavior under the conditions the waffle maker or the production plate would impose. Begin with the manufacturer’s instruction and document all changes including their effects.
Imagine a team that uses oil, increases plate temperature and shortens baking time in the same run. There’s no automatic possibility of obtaining a better waffle from any pancake mix. However, a record doesn’t show which change caused the improvement or if the result was caused by more than one change interacting with each other. Thus, to understand the effects of the change, it’s necessary to go back to a known baseline, determine which change the team intends to measure, and plan the next run. This is a synthetic example of a typical production situation and isn’t a UDTECH factory result.
The format of the batter and texture planning guide contains the more detailed description of the formulation. Commercial procurement should avoid a recommendation of a specific pancake recipe, or a single experimentally made waffle. Neither of these describes the current industrial state of batter, hold time, cleaning process or required repeatability.
The 6-Control Product-to-Trial Map is a planning worksheet
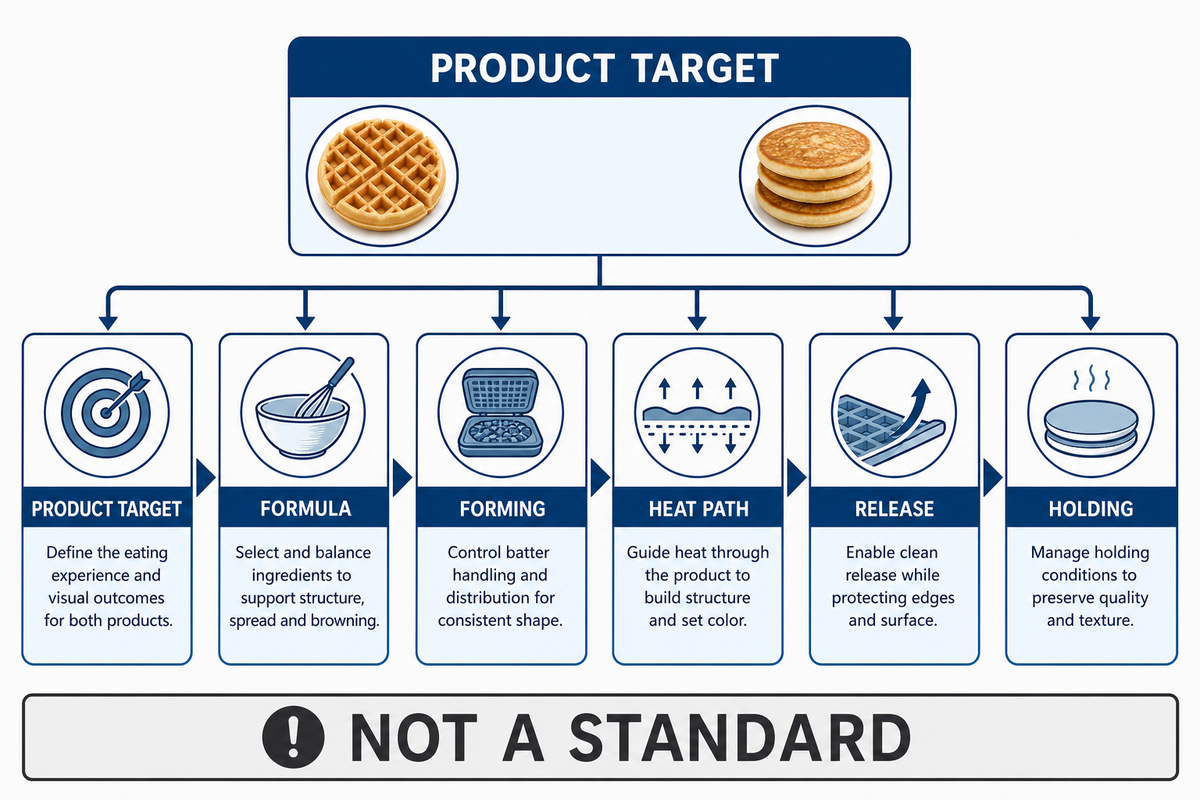
The 6-Control Product-to-Trial Map converts a general product request into six documented fields: product target, formula state, depositing or forming, heat path, release or handling, and holding or packaging. It’s a planning worksheet, not a standard, a proprietary dataset or a validated production method.
- Define the product target: record geometry, piece mass, surface, color, service texture, and acceptable variation.
- Freeze the formula state: identify recipe version, ingredient lot context, mixing method, batter temperature, and rest history.
- Describe deposit or forming: state deposit basis, cavity or spread target, and observed consistency.
- Record the heat path: capture equipment configuration, preheat state, heating settings, time, and turnover where relevant.
- Inspect release and handling: note sticking location, removal method, breakage, transfer, and cleaning or release condition.
- Judge hold or pack condition: inspect the product at the agreed service, storage, reheating, or packed-product point.
For every control, have at least one measurable observation and one acceptance boundary. “Golden waffles” isn’t a boundary until the team agrees on a reference or instrument method. “Easy release” must have the observation of complete removal without tearing given the agreed test condition. This map retains all missing data. It doesn’t provide arbitrary values.
| Control | Record | Example boundary type | Owner |
|---|---|---|---|
| Product target | Dimensions, mass, pattern, color, texture | Approved reference plus stated variation | Product and quality |
| Formula state | Version, ingredients, mix, temperature, rest | Only the named batch enters the comparison | Product and plant |
| Deposit/forming | Method, observed consistency, cavity or spread | Geometry stays inside buyer-set limits | Engineering and quality |
| Heat path | Configuration, preheat, setting, time | Condition is recorded, not assumed | Plant and supplier |
| Release/handling | Fault location, removal, damage, cleaning state | Buyer defines acceptable damage | Plant and quality |
| Hold/pack | Time, temperature, package, final inspection | Judge at the intended customer state | Quality and commercial team |
A supplier may ask for a sample before the buyer has fixed every boundary. One may justify the request for sample during the exploratory phase. Named owners should resolve the missing boundaries before the commercial acceptance run. Use the production brief input table to document the hand-off.
Match forming and heating questions to the product route
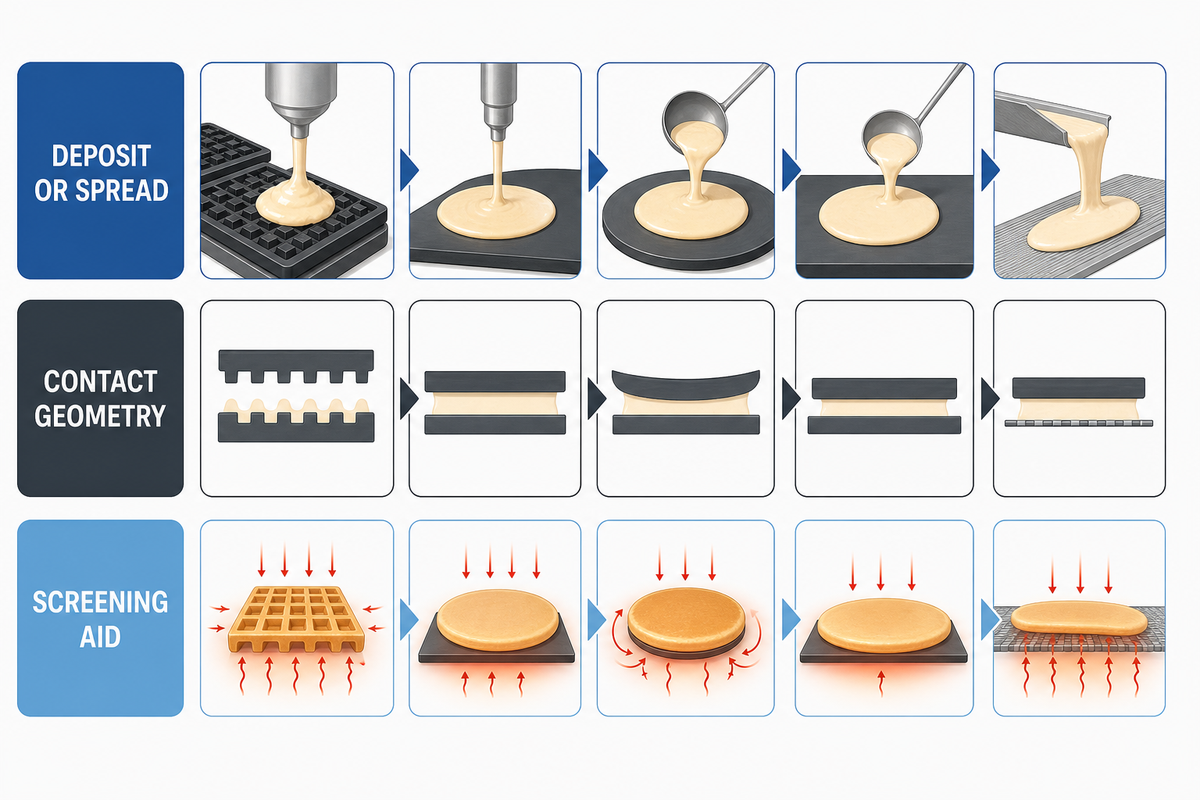
Equipment routing begins with the physical job: deposit or spread the batter, create the intended contact geometry, deliver the required heat path, release or turn the piece, and preserve it through transfer. Send the brief to an appropriate equipment family for further evaluation. Treat the route table as a screening aid, not a validated selection rule.
A plate-based waffle route is warranted when a contact geometry is patterned on two sides of the product. Review a griddle-and-depositor route when batter placement, spread, surface recovery, and turnover define a pancake. Evidence for the heating step for the shaping of a cone or a shaped-shell product is required. Neighboring crepe-type or molded products may require their own architecture.
One griddle depositor described in a Food Engineering product note travels with a cooking band, has hopper agitation, and includes programmable controls. It’s an example of bounded equipment and isn’t a universal pancake-line specification. An expired historical pancake-device patent shows batter metering and the use of a heated, rotating plate, transfer, and second-side heating. Nothing in the patent supports a UDTECH claim of ownership, current capability, or commercial performance.
When not to buy a machine from a route table
Don’t approve waffle/pancake machines, automatic pancake makers, or griddles because the product name appears in a compatible row. Stop when the buyer lacks a current reference sample, the supplier has not tested the actual formula, the quote omits the forming or release step, or downstream handling falls outside scope. A route table eliminates candidates. Only a product-specific trial and model-specific documents can be used to justify a choice.
Another machine isn’t the only alternative. It can be a different family of processes; it can include a new forming tool and a different target product. Procurement must hold the other option open until the proposed route generates the necessary geometry, texture, cleaning access, and handover.
Run controlled trials, then confirm at commercial scale
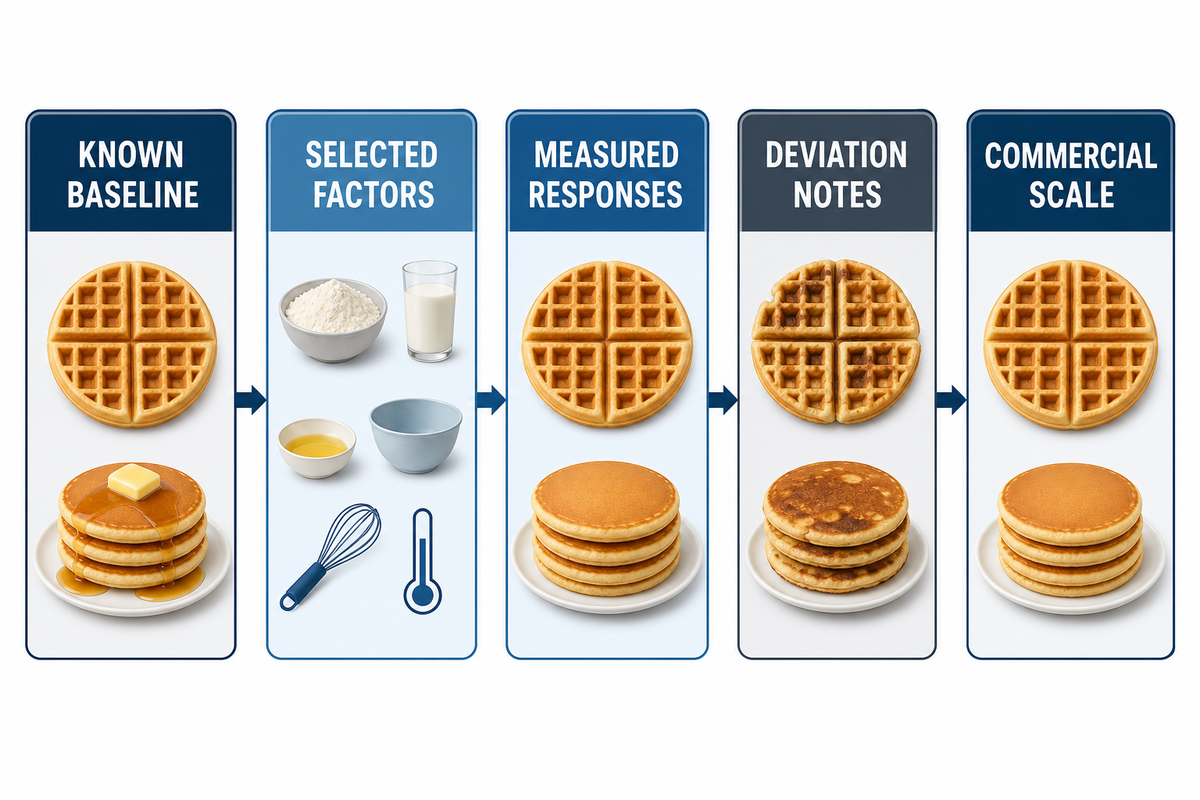
A controlled product trial begins with a known baseline, intentionally introduces changes to selected factors, measures the responses, and records inconsistencies. A subsequent check verifies, on an industrial scale, whether product behavior remains consistent in the proposed mixer, depositor, heating equipment, residence time, holding system, state of cleanliness, and the method of inspection.
As defined in the NIST Engineering Statistics Handbook, design of an experiment entails intentionally changing some process factors in order to detect their effects. In addition, this text states that machine, operator, temperature, and humidity factors may be uncontrollable, and it may be advisable to consider their interactions in the model.
“In an experiment, we deliberately change one or more process variables.”
Use a sequence that the team can audit: identify the baseline; state the response; list candidate factors; choose the factor combinations; define run order and repeats; record observations; compare against the acceptance boundary; then state the next decision. There’s no universal sample count for every waffle or pancake trial. Match the design to the risk, expected variation, available line time, and purpose of the decision.
A hypothetical version of a trial record would likely hold one recipe and one plate condition constant, compare two amounts like 55 g and 60 g, and look at the release and texture after a 15 minute hold. Those values aren’t intended to represent recommended settings. Changing formula, temperature, and hold condition together answers a different question and requires an intentional design.
| Record field | Hypothetical baseline | Hypothetical comparison | Limitations / Not suitable for |
|---|---|---|---|
| Trial batch | 5 kg | 10 kg | Not a production batch recommendation |
| Batter temperature | 20 °C | 22 °C | Not a food-safety control |
| Mix time | 180 sec | 180 sec | Equal time does not prove equal shear |
| Rest time | 10 min | 20 min | Formula response remains product-specific |
| Deposit mass | 55 g | 60 g | Not a cavity-fill specification |
| Recorded surface setting | 175 °C | 180 °C | Setpoint is not measured product temperature |
| Recorded bake time | 150 sec | 165 sec | Not a validated process schedule |
| Observed diameter | 95 mm | 100 mm | Example geometry only |
| Observed thickness | 12 mm | 14 mm | Example geometry only |
| Texture hold | 0 min | 15 min | Not a shelf-life interval |
| Room temperature | 22 °C | 25 °C | Does not define plate or batter condition |
| Relative humidity | 45% | 60% | Example environmental observation |
| Observed defect share | 2% | 6% | Not an acceptance limit |
| Cooling observation | 10 min | 20 min | Not a packing release rule |
| Recorded line dwell | 3 min | 4 min | Not a commercial residence-time claim |
Replacing all the made-up values with actual values from the recipe, equipment, and the trial plan will fill out the table. This table won’t show an optimal recipe, but it will show why each result needs a value, unit, and boundary.
Scale-up also adds a checkpoint. As described in the article, https://extension.okstate.edu/fact-sheets/scaling-up-your-food-process, by Oklahoma State University Extension , food systems can behave differently at larger scale, and surface-area-to-volume relationships can alter mixing and heating. Time needed to mix and heat the food can also change. Time needed to hold the food, as well as air incorporation and burn-on, can change with material handling and cleaning. A kitchen or even a pilot batch isn’t enough to show that the operating window is the same.
One development trial doesn’t validate applicable preventive controls. For covered United States facilities, 21 CFR 117.160 states validation requirements for applicable preventive controls and then exempts food-allergen controls, sanitation controls, recall plans, supply-chain programs, and certain justified controls from the requirements of this section’s validation. The Buyer’s qualified Food Safety Owner is responsible for what applies; a product trial can’t make this determination.
The controlled-change trial record helps differentiate the baseline from the following comparison. If capital reviewers object to another trial, show the unresolved scale-transfer variables. A repeat on the commercial equipment poses a different question from a successful bench sample.
Diagnose sticking, weak structure, and uneven color without single-cause guesses
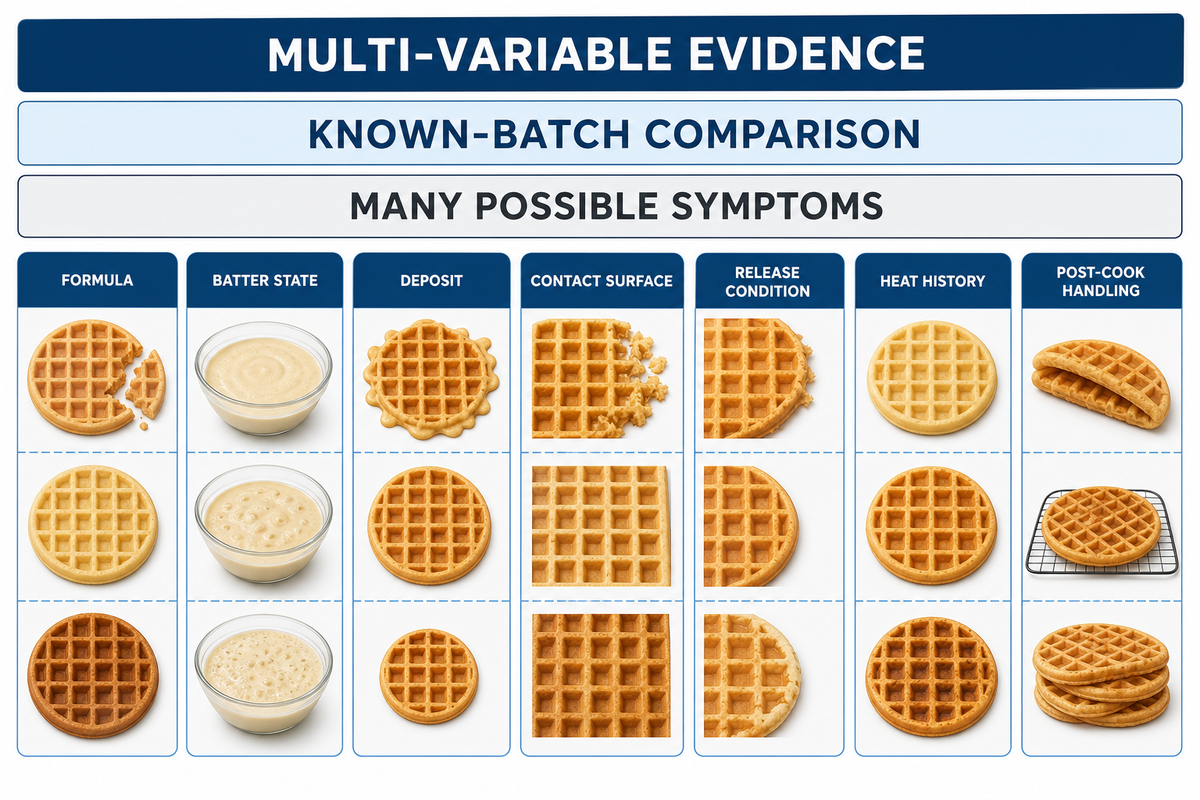
Prior to changing the recipe or the machine, defect analysis requires comparison of evidence across formula, batter state, deposit, contact surface, releasing condition, heat history, and post cooking and handling.
| Observed symptom | Competing causes | Measure next | Limitations / Not suitable for |
|---|---|---|---|
| Sticks across the plate | Batter, surface, release, heat, cleaning | Fault map and known-batch comparison | One release-agent change cannot isolate all causes |
| Sticks at one corner | Deposit distribution, plate condition, alignment | Location pattern over repeated pieces | Whole-recipe change may hide a local fault |
| Weak waffle grid | Fill, structure, opening time, handling | Section, mass, release, and break point | Color alone cannot explain structure |
| Pancake spreads too far | Batter state, deposit, surface, delay | Temperature, rest history, and diameter | Viscosity guess without method is weak evidence |
| Uneven color | Deposit, contact, heating zone, turnover | Mapped surface pattern and actual settings | Average color can hide a zone fault |
| Pale center | Thickness, heat path, residence | Section condition and location-specific color | External color cannot release the center |
| Softens during hold | Formula, cooling, humidity, package, topping | Timed checks under stated conditions | Exit-line texture is insufficient |
| Breaks at transfer | Structure, release, timing, conveyor handoff | Before-and-after good-piece counts | Machine-exit sample misses transfer loss |
| Batch drift | Ingredients, mixing, wait time, environment | Batch identity and time-stamped conditions | Single final sample hides the drift path |
Sticking is one of many possible symptoms and may result from several causes which may arise simultaneously. A direct approach to sticking is to try increasing the oil. However, the trial members may not have cleaned the plate adequately, the batter may have been left for a longer time, and the equipment may not have recovered its stated preheat condition. The next result may mix four different causes. Keep the recipe fixed, take a photograph of the defect, record the state of releasing and cleaning equipment, and describe a known state prior to changing another factor. This represents a constructive failure scenario and isn’t a real case.
Do
- Map where the defect appears.
- Retain the batch and setting record.
- Measure at the intended hold point.
Do not
- Blame the heater from color alone.
- Change formula and settings without a plan.
- Copy another study’s sticking rate as a limit.
The pilot-scale study reviewed relied on a process consisting of 30 waffles per recipe and observed materially different sticking behavior under different formulations. This type of evidence can certainly aid the diagnosis. However, it doesn’t provide a standard limiting sticking behavior, temperature, and the cleaning method applicable to other lines. To complement the evidence, use the batter observation record, and provide the actual process conditions.
A texture pass is not a process-safety, allergen, or sanitation release
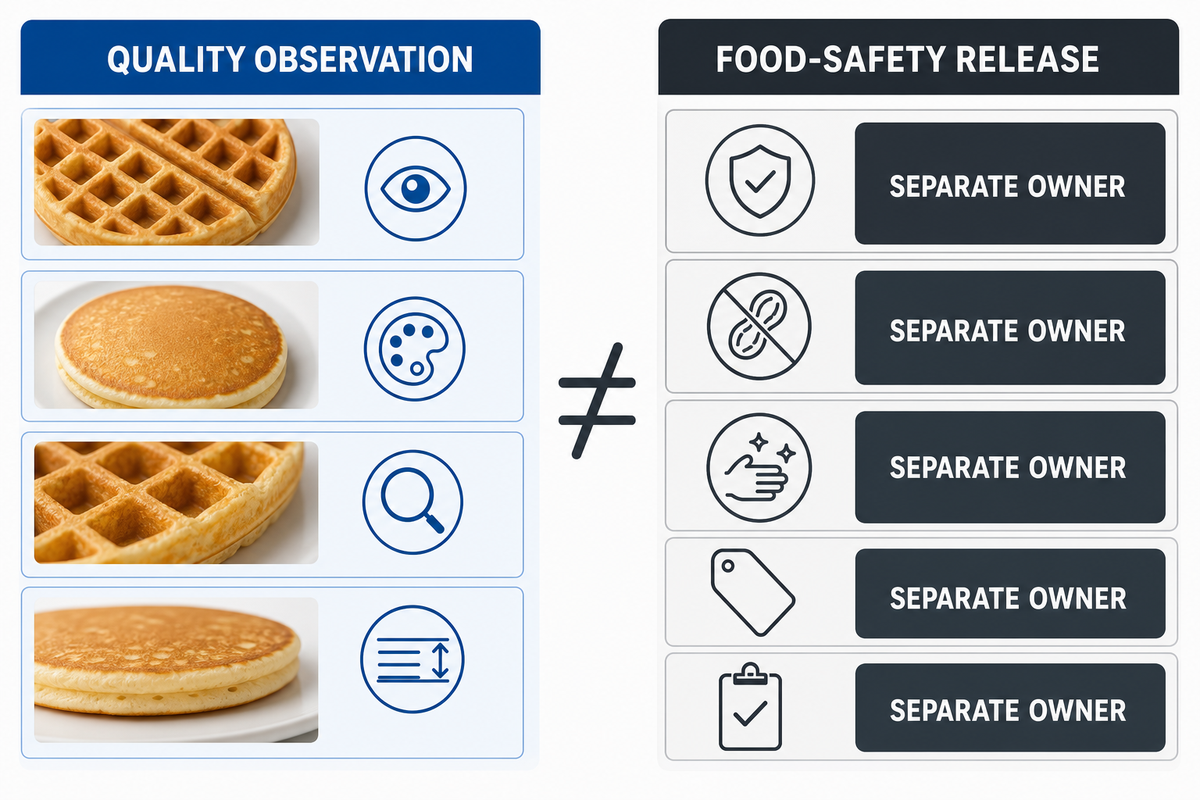
Evidence of product quality is limited to observations of waffle, pancake, clean releases or adequate color. Those observations can’t determine control of raw material hazards, allergen cross contact, control of equipment, effectiveness of sanitation, accuracy of labels, or food safety release. Each must have a responsible owner, domain, methodology and retained evidence.
Raw-material boundaries begin before baking. The United States Food and Drug Administration’s page on flour safety says flour is a raw material that may contain pathogens and states that grinding doesn’t inactivate harmful pathogens. Page content is designed for the consumer and thus isn’t an industrial lethality schedule. Hazards and controls need to be identified by a qualified food safety team for the actual formulation, equipment, process history, intended use and jurisdiction.
Sanitation and allergen issues are tied to manufacturing decisions. Introducing a new formulation can introduce a major allergen. Design and scheduling can impact the cross contact risk. Food-contact design, access, cleaning procedure, verification, and records affect whether the line is ready for the next product. For the scope of U.S. facilities, 21 CFR Part 117 addresses these concerns, yet the regulation doesn’t validate a specific waffle iron, pancake machine, or cleaning protocol.
| Trial observation | What it can show | What it cannot show | Owner and evidence |
|---|---|---|---|
| Desired crispness | Texture under stated conditions | Pathogen control | Food-safety team and control records |
| Clean visual surface | No visible residue at inspection | Sanitation effectiveness | Sanitation owner and verified procedure |
| Easy product release | Release in the test state | Hygienic cleanability | Engineering and food-safety review |
| Accepted ingredient batch | Identity of tested inputs | Supplier control for future lots | Supply-chain and quality records |
| No visible cross-contact | Visual observation only | Allergen control effectiveness | Facility allergen-control evidence |
| Correct sample label | Trial identity | Finished-food label compliance | Regulatory and label review |
| Stable 20-minute hold | Quality at one stated interval | Shelf-life or distribution safety | Quality and food-safety programs |
| Repeated good pieces | Observed repeatability in the run | Commercial validation at another scale | Plant, supplier, and acceptance test |
| Supplier certificate | Claim within its stated scope | Performance in the buyer’s application | Buyer verification and process evidence |
A customer may request “certification of the changeover.” This needs to be addressed in two parts. The supplier can document the material of construction, surface finish where appropriate, access, disassembly, and the test or certification scope as well as the proposed cleaning method. Process-specific cleaning remains the food manufacturer’s responsibility and must be verified for the real soils, allergens, tools, utilities, sequence, and product risk.
The ingredient function reference explains how formula adjustments can influence product behavior and notes that equipment selection does not authorize an ingredient or validate a label. Such product-development guidance does not replace the buyer’s food-safety, allergen, labeling, or regulatory review. Therefore, it’s of utmost importance that those records are kept distinct from the first trial onward.
Prepare a site-fit checklist before any procurement discussion
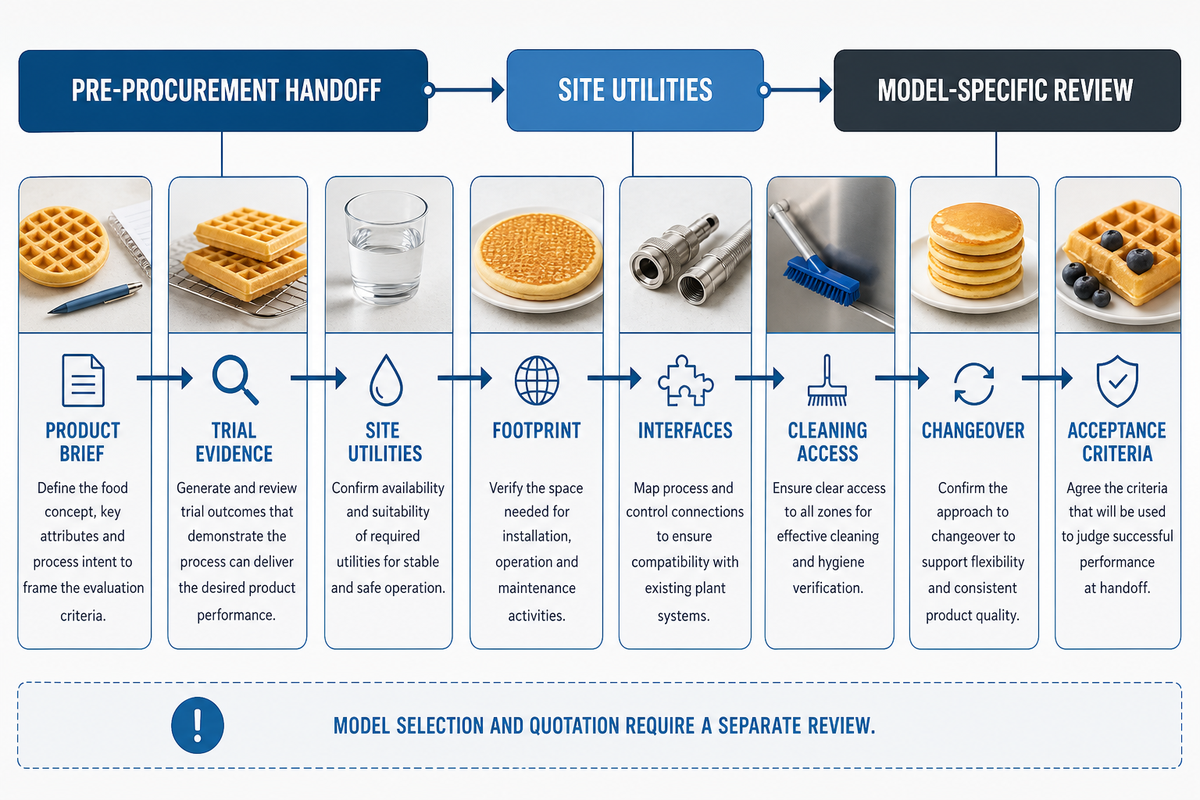
A pre-procurement handoff record should explain the product brief, trial evidence, target output basis, site utilities and available footprint, upstream and downstream interfaces, cleaning access, production order, allergen changeover concerns, and acceptance test criteria. This checklist supports a later commercial discussion; it does not replace the site-readiness, utility, line-sizing, or model-selection pages that own those detailed buying decisions.
This output is based on the target. Does it mean deposited parts, released parts, good parts following the transfer, or packed saleable product? Give the reference product and the permitted variation. Then, provide an electric supply, heating source, compressed air, exhaust, water or drainage as needed, install clearances, access for the operator, if necessary, load on the floor, controls interface, and the supply constraint.
Hygienic design is included in the same handoff. An EHEDG page on hygienic-design scope describes equipment, links between equipment, and operating utilities as part of clear buyer-supplier expectations during development and handover. It provides guidance, not a definition of a universal machine. There’s another EHEDG test-methods page that states that a test of hygienic or aseptic design doesn’t indicate performance in a specific application and leaves the food processor manufacturer to devise the appropriate cleaning protocols for the process.
Consider an example with a quote on pieces per hour with no allowance for set up, cooling, transfer or packing. If rework due to downstream impacts damages 3 pieces of a 50 piece example, then the estimated loss would be 3/50 = 6% (the example shows illustrative numbers and is used to set the boundaries of acceptable limits). It shows why the buyer should define where output is counted and retain before-and-after observations.
Plant teams may argue that utility details can be addressed once the purchase is finalized. This may not be possible if the site is missing the necessary service, access, exhaust path, controls interface, or a means for cleaning. Instead of copying values from other lines, provide model-specific load sheets and drawings. Ask who supplies each conveyor, guard, extraction point, inspection device, recipe system, and interface signal.
Changeover varies by product. Note the outgoing and incoming formulas, major allergens, contact surfaces, removable parts, cleaning tools, verification method, production sequence, and evidence the buyer is looking for. You may wish to review a hygienic-design document or certificate, but keep in mind that they can’t prove the cleaning performance for the buyer’s soil and operating practices.
Use the baking texture science hub to answer related product-quality questions. The existing production guide and tools provide planning context for the product brief and trial discussion; model-specific machine selection, capacity, utility needs, specifications, and commercial scope still require a separate review. This article sets up the evidence to support the conversation that follows.
Outlook: what automation can record, and what it cannot validate
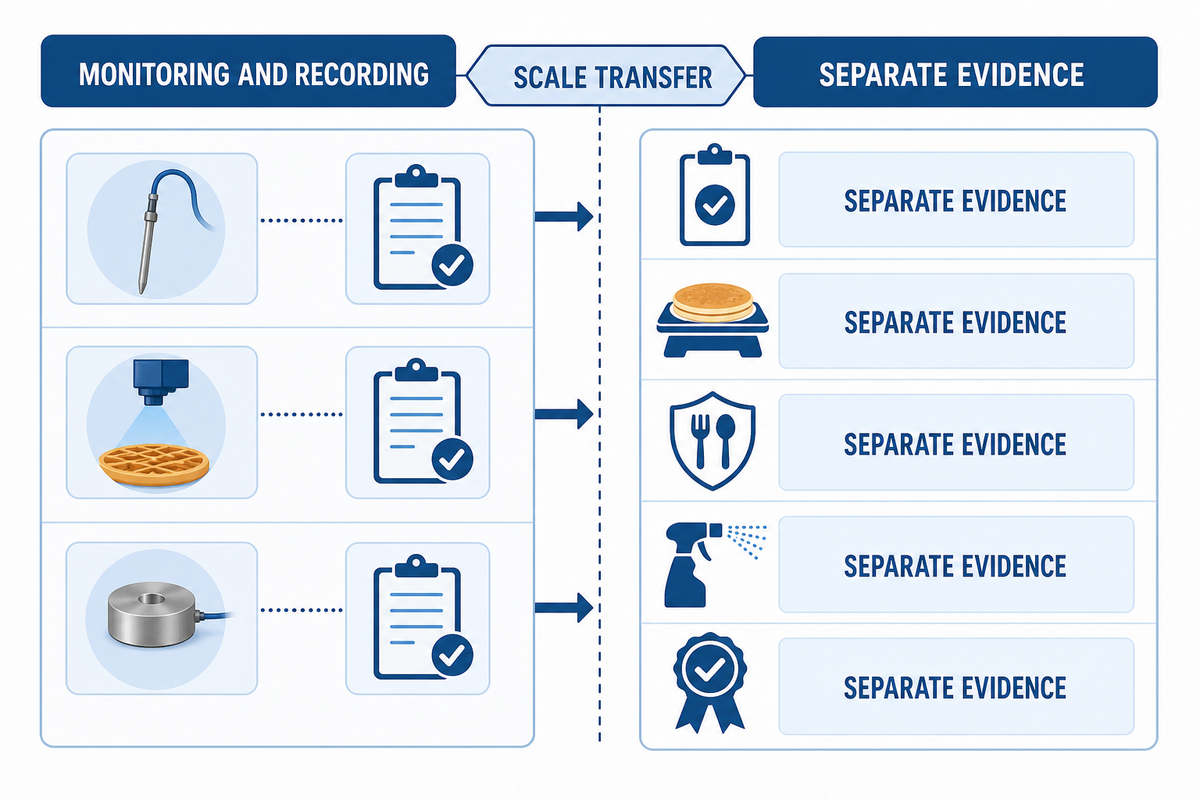
The proposed system can automate setting, monitoring, triggering alarms and recording defined process conditions if the system incorporates the requisite sensors, controls, interfaces, and data management. Automation can’t define the right formula, prove scale transfer, release food safety, verify cleaning performance, or accept a commercial line without separate product-specific evidence.
An equipment-supplier outlook for 2026 published in 2025 looks at automation, standardized interface, modular design, cleanability, and sustainability. Consider this as attributed supplier context. The reviewed sources didn’t provide an independent before-and-after dataset to show that the introduction of automation improved the quality of waffle and pancake.
The current keyword series comprises 12 consecutive months. While it captures seasonal trends within this 12-month window, it can’t support a year-over-year market-growth claim without the prior comparison period. Procurement must reject a capital case that relies on a generic growth forecast or an increase in search volume. The case should be built around a specific product, the buyer’s demand and acceptance assumptions, site fit, and verified commercial scope.
For a 2026 project, ask four direct questions: which variables can the system set; which conditions can it measure; which deviations can it alarm on; and which records can it export with batch identity and timestamps? Decisions that fall outside the control system must also be documented. Formula approval, applicable food-safety controls, cleaning verification, scale-up confirmation, and final acceptance each need their own owner.
Key takeaway
A production-ready waffle or pancake decision joins six documented controls to a controlled trial, a commercial-scale confirmation, and a separate safety and procurement review.
Frequently asked questions
Can the same batter be used for waffles and pancakes?
A single batter can make both formats in some cases, but it should not be assumed to meet both finished-product targets under both documented production conditions.
Waffles must fill and release from patterned heated surfaces and may need a crisp shell after holding. Pancakes normally spread and set on a griddle before turning or further heating. Define geometry, color, texture, hold state, and release, then test formula, deposit mass, surface condition, heat, time, and post-cook handling under recorded conditions.
Can pancake mix be used in a waffle maker?
Some pancake mixes can produce a waffle, but the result is not guaranteed to meet commercial release, color, texture, or holding requirements for the intended process.
Start with the mix supplier’s directions and a defined target. Record every change to added water, milk, egg, butter or oil, plus batter temperature, rest time, amount of batter, plate condition, preheat state, bake time, release, and texture after the required hold. A pleasing homemade result doesn’t prove behavior in commercial waffle equipment.
What is the best recipe for waffle and pancake batter?
No single recipe is best for both products; the right formula meets a stated target under the intended process, service conditions, and intended hold state.
Compare candidate formulas through planned trials. Measure the attributes that matter, such as piece mass, dimensions, surface definition, color, release, texture at service, and stability after holding. Keep raw-material hazards, allergen controls, sanitation, labeling, and preventive-control decisions separate from sensory acceptance. Those decisions may reconnect operationally, but they don’t share one universal pass result.
Why do waffles become crisp while pancakes usually stay soft?
Waffles usually contact patterned hot surfaces on two sides, while pancakes commonly cook against a griddle with an initially open upper surface before turning or further heating.
Two-sided patterned contact often changes surface heating and moisture loss. Formula and holding still decide whether the finished waffle stays crisp.
How do you scale a kitchen waffle or pancake recipe for production?
Scale-up begins by converting the kitchen result into measurable targets, then confirming the product again on the proposed commercial process at the intended production scale.
Record ingredient basis, mixing sequence, batter temperature, rest time, deposit mass, contact surfaces, heat conditions, cook time, release method, dimensions, color, texture, and holding state. Establish a baseline and use controlled comparisons. Larger batches can change mixing energy, hydration, aeration, temperature, residence, and cleaning behavior, so multiplying ingredient quantities is only the arithmetic step. Utilities, line interfaces, safety controls, and supplier acceptance testing need separate evidence and owners.
Ready to turn the target into a supplier brief?
Take the reference product, six-control worksheet, trial record, and site questions to the UDTECH waffle and pancake production overview. Request a model-specific scope and product trial; don’t rely on category-level claims.
Source and scope note: This article uses public regulatory, academic, extension, association, patent, trade, and supplier material plus a clearly labeled editorial framework. It reports no UDTECH factory measurement, model capacity, patent ownership, investment, site area, customer result, or validated application performance. Regulations apply only within their jurisdiction and facility scope. Product-quality acceptance and food safety release, as well as cleaning verification and equipment conformance, must also be reviewed on a case-by-case basis.
References & Sources
- Stickiness of waffles: Interplay between ingredients and the baking process peer-reviewed study.
- What is experimental design? NIST Engineering Statistics Handbook.
- 21 CFR 117.130: Hazard analysis Electronic Code of Federal Regulations.
- 21 CFR 117.160: Validation of preventive controls Electronic Code of Federal Regulations.
- Handling Flour Safely United States Food and Drug Administration.
- Scaling Up Your Food Process Oklahoma State University Extension.
- EHEDG white paper on GFSI hygienic-design scope European Hygienic Engineering & Design Group.
- EHEDG test methods and application limits European Hygienic Engineering & Design Group.
- Griddle depositor product note Food Engineering.
- EP0214188A1 pancake apparatus publication historical third-party patent record.
- Foodservice equipment trends to watch in 2026 attributed supplier outlook.