Two guide modules
Waffle and Pancake Guides for Batter Texture & Production.
The textures produced with commercial waffles and pancakes can simplify production teams’ descriptions of batter texture. Document the product target, formula context, mixing history, holding conditions, method of deposit, cooking surface, result of release, cooling, and pack format. Discuss these points prior to addressing a production line.
This text is intended for plant managers, product developers, quality teams and procurement staff who are transitioning from a pilot batch to either commercial waffle production or a pancake making machine project. This text does not provide a recipe, nor does it state that one thickness is applicable for all products.
Discuss Your Production Brief
Put the actual product target and the conditions that pertain to your observation. A number without a method and context is not sufficient enough to make a production decision.
Discuss Your Production Brief
Batter context before equipment discussion
Waffle and pancake use cases kept distinct
Three browser-based preparation tools
A clearer brief for an engineer
Waffle & Pancake Processing Guides
Commercial Waffle and Pancake Guide Scope
Consumers combine searches for pancake recipe, waffle recipe, and equipment on the same page. This may result in a poor production brief as “best waffle,” “fluffy,” and “crispy” describe desired end results without noting the production conditions for these results.
Consumer language translated into production inputs
Amateur production advice may tell a cook to whisk dry ingredients, fold egg whites at soft peaks, add melted butter at room temperature, preheat a waffle iron, or thicken pancake mix. It may discuss baking powder, baking soda, buttermilk, gluten, wet ingredients, 1 cup measures, blueberry or chocolate chip additions, whipped cream, maple syrup, another topping, or breakfast serving.
These descriptions may apply to a waffle mix or pancake batter, but they do not provide a repeatable method of commerce. The production record must explain what “make the batter,” “make waffles,” or “make pancakes” means in terms of measured processes.
Decision language kept separate
This guide covers waffle batter consistency, pancake batter consistency, waffle sticking problems, and the production issues associated with them, but it will not take a Belgian waffle / fluffy pancake or syrup-ready finish and turn it into a universal machine setting.
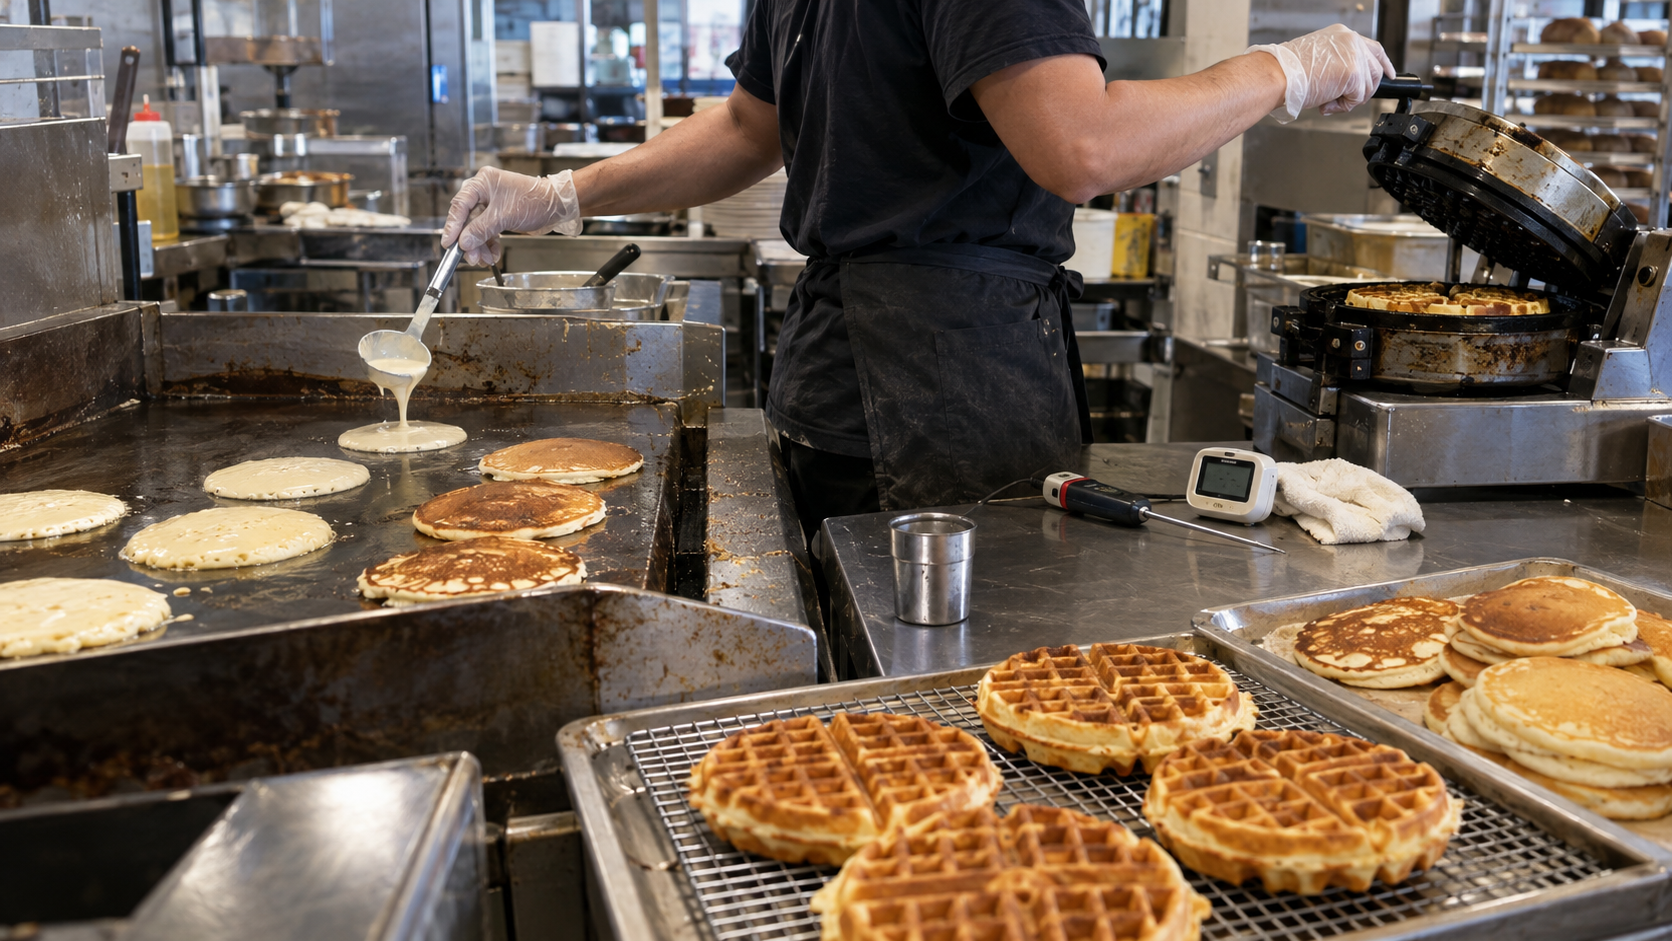
Unlike a consumer recipe, this guide does not address the waffle vs pancake batter issue based on thickness. A pancake and waffle line should describe the waffle maker or cooking interface, and the trade-off is also related to formula, aeration, time, temperature, and heat transfer, as well as the plate condition and holding.
Formula and Context Inputs Worth Recording
Batter sticking is observed when the formula is unchanged. The written ingredient list is just one part of the context. Product developers and plant operators must note the formula and process history before comparing two trials.
Formula identity
Record the formula revision, flour or starch system, water basis, fat system, sweetener, salt, leaven, emulsifier, egg component, and any inclusion. Note substitutions instead of treating two versions as the same batch.
Mixing history
Record ingredient order, stage times, speed, rest, transfer, and operator. Different operators can turn the same written recipe into different observation contexts.
Temperature and time
Record batter temperature at the stated observation point, room conditions when relevant, time since mixing, time in a hopper or vessel, and any stop-start period. The same batter can behave differently after holding, transport, depositing, or a change in plate condition.
Measurement method
Name the method, instrument or cup geometry, sample amount, test temperature, number of repeats, and units. A published waffle study used a 100 mL flow cup with a 10 mm outlet and triplicate readings; that is a study method, not a universal factory target.1
Product and formation
Identify the intended form, deposit amount, spread, inclusion, contact geometry, and release method. A lump, bubble pattern, or thick batter observation matters only in relation to that product.
Post-cook path
Record cooling, stacking, freezing or holding, and pack format. Crispness at release may change after moisture migration, so name the observation point.
Production & Quality Control
Process Interactions Behind Texture and Release
A modified operator, hold time and adjusted cooking surface can yield different results even with no changes to the formula sheet. The table below shows what causes remain unassigned and indicates which paired observations help production teams plan a controlled trial.
Controlled Trial Observation Parameters
Observed issue
Context to record
Next comparison boundary
Irregular flow or spread
Method, sample temperature, time since mixing, shear and transfer history
Hold formula and deposit point constant; change 1 declared variable
Sticking at release
Surface condition, cleaning state, release aid, contact time, temperature record
Do not assume batter consistency is the only cause
Pale or uneven color
Deposit distribution, surface contact, heat recovery, time and product position
Compare the same observation point across at least 2 repeats
Soft exterior after cooling
Release texture, cooling duration, stacking, humidity and packaging state
Separate cook result from post-cook moisture movement
Dense or irregular structure
Formula revision, leaven, aeration, mixing, rest time and deposit action
Use one controlled change rather than several simultaneous fixes
Variable product weight
Deposit setpoint, actual sample weights, hopper level and batter condition
Record both target and observed values with units
Good release but poor pack texture
Cooling, stacking, freezing, reheat method and pack barrier
Test the finished distribution condition, not only the hot product
Trial result cannot be repeated
Missing timestamps, units, instrument, sample point or process revision
Rebuild the observation record before changing equipment
Batter Context Capture Sheet
The Batter Context Capture Sheet provides a comparable report when a general complaint of texture is documented. The sheet does not diagnose, recommend a solution, or make a judgment or document a result.
Active Field
Product target
Product target
What to capture
Style, dimensions, mass, color, bite, exterior and serving or pack state
Why the field matters
Defines the observation point without forcing a universal texture target
Formula revision
What to capture
Revision ID, ingredient lots, substitutions and inclusion details
Why the field matters
Prevents different formulations from being compared as one batch
Mixing record
What to capture
Order, stage times, speed settings, rest time and operator
Why the field matters
Links the written formula to its actual preparation history
Time and temperature
What to capture
Batter temperature, room context, time since mix and hold duration
Why the field matters
Makes a flow or release observation reproducible enough to compare
Measurement method
What to capture
Instrument or cup, geometry, sample amount, units and repeat count
Why the field matters
Stops unlike readings from being treated as equivalent
Deposit context
What to capture
Target and actual amount, deposit pattern, transfer route and hopper state
Why the field matters
Separates delivery behavior from cooking behavior
Cooking context
What to capture
Surface identity, temperature record, contact time and recovery condition
Why the field matters
Connects texture and color observations with heat-transfer context
Release result
What to capture
Release action, residue, sticking location, plate state and intervention
Why the field matters
Provides a neutral account of waffle sticking problems
Post-cook path
What to capture
Cooling, stacking, freezing, holding, packaging and reheat condition
Why the field matters
Locates where crispness or softness changed
Trial decision
What to capture
Single variable changed, constants held, repeat count and next review owner
Why the field matters
Keeps the comparison controlled and assigns the next decision
Browser-based observation record
Once ten context fields have been filled, blanks can be recorded and a neutral record can be copied. The tool does not store information on a server and is not intended to aid in the diagnosis of batter.
Project Inputs That Shape Equipment Scope and Validation
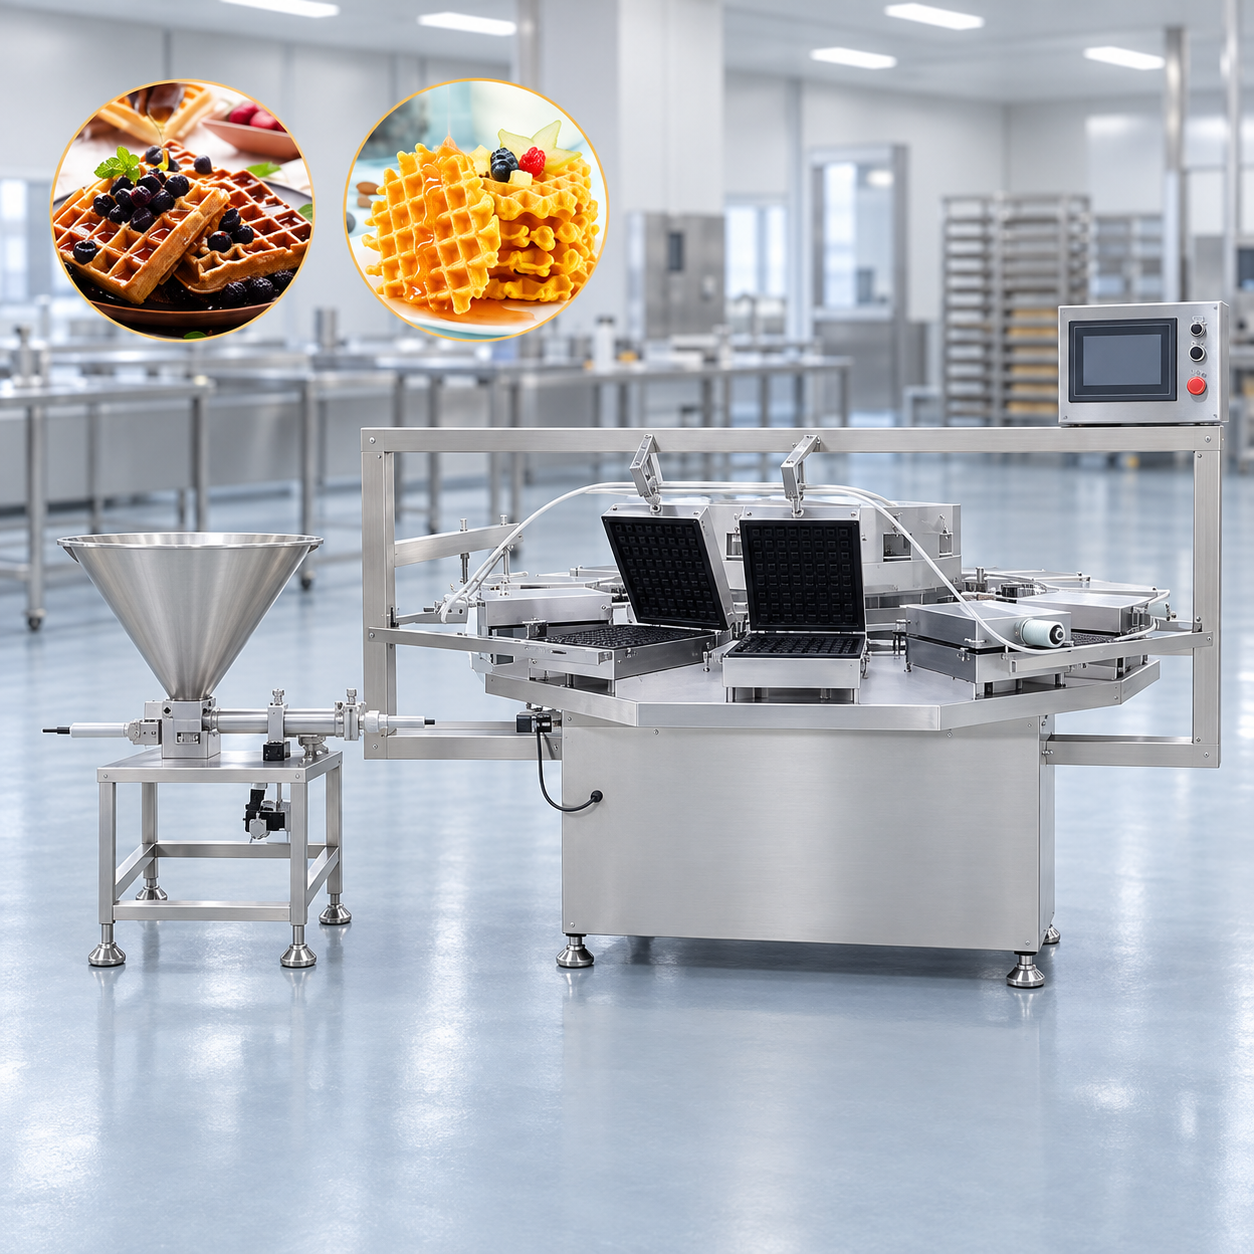
The cost and timing of a product are driven by the process interfaces, utilities, hygiene, and the control, test, training, install, and support scope. The equipment’s cost and timing will be driven by these inputs, so in this guide, no prices, savings, payback, minimum order, or warranty, and delivery can be guaranteed.
NIST recommends that manufacturers evaluate the location, utility availability, adjacent equipment, training, use, maintenance, and end-of-life when purchasing equipment 5. That vendor-neutral frame helps procurement compare scope rather than compare headline machine prices alone.
Production brief input table
Check if the project brief addresses product, throughput, interfaces, site, hygiene, controls, testing, and commercial handover. The output indicates the absence of inputs; it does not evaluate or select a machine.
Cost and scope input table
Information to bring
Required Product Specifications
Product form, target dimensions and weight, formula family, inclusions, finished-state criteria
Decision it supports
Application Framing
Frames the application instead of guessing from a machine name
Information to bring
Throughput & Scheduling Data
Required good output, schedule, shifts, changeovers, yield basis and growth case
Decision it supports
Actual Output Calculation
Separates usable output from nominal speed
Information to bring
Pre-Processing Needs
Mixing, holding, transfer, temperature control, inclusion handling and batter delivery
Decision it supports
External Interface Mapping
Reveals interfaces that may sit outside one machine
Information to bring
Post-Processing Routing
Release, cooling, freezing, inspection, stacking, packing and rework route
Decision it supports
Workflow Continuation
Shows where the product must go after cooking
Information to bring
Facility & Site Context
Available footprint, access route, floor and drainage context, utility data and local restrictions
Decision it supports
Hidden Cost Prevention
Prevents site work from remaining invisible in a quote comparison
Information to bring
Sanitation Requirements
Allergen profile, cleaning method, zoning, product sequence and verification expectations
Decision it supports
Food-Safety Definition
Defines the changeover and food-safety discussion
Information to bring
Automation & Signals
Operator roles, recipe management, data needs, alarms and upstream or downstream signals
Decision it supports
Engineering Pre-Planning
Identifies control interfaces before detailed engineering
Information to bring
Testing Protocols
Trial material, sample criteria, repeat count, witnesses, records and approval owner
Decision it supports
Procurement Usability
Makes a test result usable for procurement
A common assumption is that the purchase of the cheapest machine delivers the best project cost. This assumption may conceal hidden costs related to utilities, ancillary work, validation, training, and integration. Send your application inputs for details.
Production Validation, Allergen and Hygiene Checkpoints
Cleaning between product runs can be as much about hazard control as it is about convenience. For projects under the U.S. Food Rules, 21 CFR 117.135 prescribes preventive controls in a written food safety plan as part of a food safety hazard analysis when hazards are identified that require control.3
The FDA identifies nine major food allergens in the United States: milk, egg, fish, crustacean shellfish, tree nuts, peanuts, wheat, soybeans, and sesame. 4 Advisory label wording cannot be used as a substitute for good manufacturing practices and controls for cross-contact.
Validation questions for the project team
- Define the finished-state criteria: Product size and weight, appearance, structure, bite/chew, post-cook position, and release.
- Set the trial conditions: Formula change, sample size, run state, measurement method, number of repetitions, cleanliness state, and order of runs.
- Food safety ownership for hazard analysis, the allergen matrix, sanitation, verification, labeling, and product release must be defined.
- Agree on the evidence package: Measurements, photos, samples, records, deviations, and approvals.
Food-contact context
List product-contact surfaces, transfer points, residues and cleaning access that the project team needs to review.
Changeover context
List product order, allergen transitions, cleaning steps, inspection points and release authority.
Jurisdiction context
Confirm which laws, codes, customer standards and facility rules apply; the United States references here do not replace local review.
Sample context
Link every sample result to the formula revision, process state, timestamp, units and acceptance owner.
From Batter Notes to an Equipment Conversation
A controlled-change record describes one controlled variable and keeps the others the same. It is a recorded discussion aid and cannot be a cause for acceptance.
Describe the intended product, the finished state target, the route of serving or packaging, and the location of the observation.
1
Record Details
Record the formula change, mixing, temperature, time, deposit, contact surface, release, and cooling as well as the hygiene state.
2
Assign Inputs
While missing inputs remain visible, assign each input an owner and the next collection point.
3
Plan Comparison
Plan one controlled comparison with one variable change, named constants, repetitions, and records.
4
Interpret Record
Staff from product development, production, quality, procurement, and engineering must interpret the record based on their areas of responsibility.
5
Additional Criteria
Add output, interfaces, utilities, cleaning, controls, trial criteria, site limits, and commercial questions.
Waffle & Pancake Production Tools
SYS.01
Batter Observation Record
This tool organizes observation context. It does not diagnose a cause, recommend a correction, score the batter, or accept a product.
SYS.02
Controlled-Change Trial Record
Declare one change and the conditions that stay constant. This tool plans a record; it does not infer cause, set a process target, or accept a result.
SYS.03
Production Brief Input Table
Describe what the project team already knows. The checker lists missing input groups; it does not select a machine, calculate capacity, estimate price, or approve a project.
Waffle and Pancake Batter FAQs
There is no universal value for every product and process. Record the target waffle style, formula, measurement method, sample temperature, hold time, deposit method, cooking geometry, release, and finished-state observation before comparing thickness.
Not as a blanket rule. A waffle and a pancake differ in intended form, formation, contact geometry, heat transfer, release, and serving or pack route; compare defined products rather than relying on one adjective.
Name the measurement method and sample point, then record formula revision, temperature, elapsed time, mixing and transfer history. Use at least 2 comparable observations before discussing a trend, while leaving diagnosis to the assigned technical team.
The formula may be unchanged while the time, temperature, mixing, deposit, surface condition, cleaning state, release practice or heat recovery has changed. Record the first, middle and later run observations before assigning a cause.
No. A peer-reviewed waffle study used 100 mL, a 10 mm outlet and triplicate measurements within its own method.1 Reuse that method only after a qualified team confirms that it fits the product and decision.
Those values describe conditions in one published experiment using 15 mL samples.1 They are not a default for another formula, plate, machine, plant or finished-product target.
For a United States project, list which of the FDA’s 9 major allergens are present, the product sequence, cleaning method, verification, labeling responsibility and release owner.4 Confirm every other market and customer requirement separately.
No. FDA explains that advisory statements are not a substitute for good manufacturing practices and precautions against cross-contact.4 The plant’s applicable food-safety plan controls the decision.
Send 1 defined product brief covering formula family, finished criteria, required good output, schedule, upstream and downstream interfaces, utilities, footprint, hygiene, controls, trial plan, training and installation scope. The browser tool marks gaps without estimating a price.
No. Machine speed does not answer whether the finished product meets its intended texture and release criteria. Tie output discussions to a defined good-product basis, test conditions, repeat count and written acceptance owner.
The Controlled-Change Trial tool is built around 1 declared change, named constants and a planned repeat count. A qualified team may design a different experiment, but several untracked changes weaken causal interpretation.
Prepare the product target, formula context, deposit and cooking path, required good output, plant constraints, utilities, hygiene boundary, controls, downstream interfaces and trial criteria. Use the 3 linked browser tools to organize those inputs before opening the contact window.