Baking Science for Industrial Ingredients and Texture Control
Baking science explains how ingredients, mixing, heat and mass transfer create structure, browning, aroma, moisture and texture. An industrial baker uses this science to develop a way to consistently connect a desired product to a repeatable process.
-
Formula
Ingredient identity, ratio, lot and sequence
-
Transformation
Gas generation, protein change and starch behaviour
-
Heat & Moisture
Surface contact, internal movement and evaporation
-
Structure
Cell opening, setting, release and cooling
-
Outcome
Colour, crispness, tenderness, flavour and shelf-life target
- 1 set Minimum order quantity
- 30–35 days Production lead time
- T/T or L/C Payment method; schedule stated in the quotation
The Baking Outcome Evidence Chain
The science of baking is useful to a production team when each final product can be traced back to five layers of evidence. A single fixed sensor can show one location, but it may leave upstream and downstream causes unresolved. Because that gap can hide a formula, heat-transfer or cooling risk, UD Company keeps the FDA hazard-analysis context and finished-product record as separate evidence, not interchangeable shortcuts.
What enters the process
Flour and protein content, gluten potential, starch, sugar, reducing sugar, fat, cream, egg, water and leavening agent choices.
What changes
Baking soda or baking powder can release carbon dioxide, while mixing and heat alter dough or cake batter structure.
How energy moves
Heat is transferred through the product while water content moves and evaporates under product-specific reaction conditions.
What sets and releases
Gas cells, a gluten network, starch behaviour and cooling determine whether the product holds, bends, cracks or releases.
What the buyer accepts
Colour, chewy texture, crispness, aroma compounds, flavor profile, break force, moisture and shelf life belong in the acceptance record.
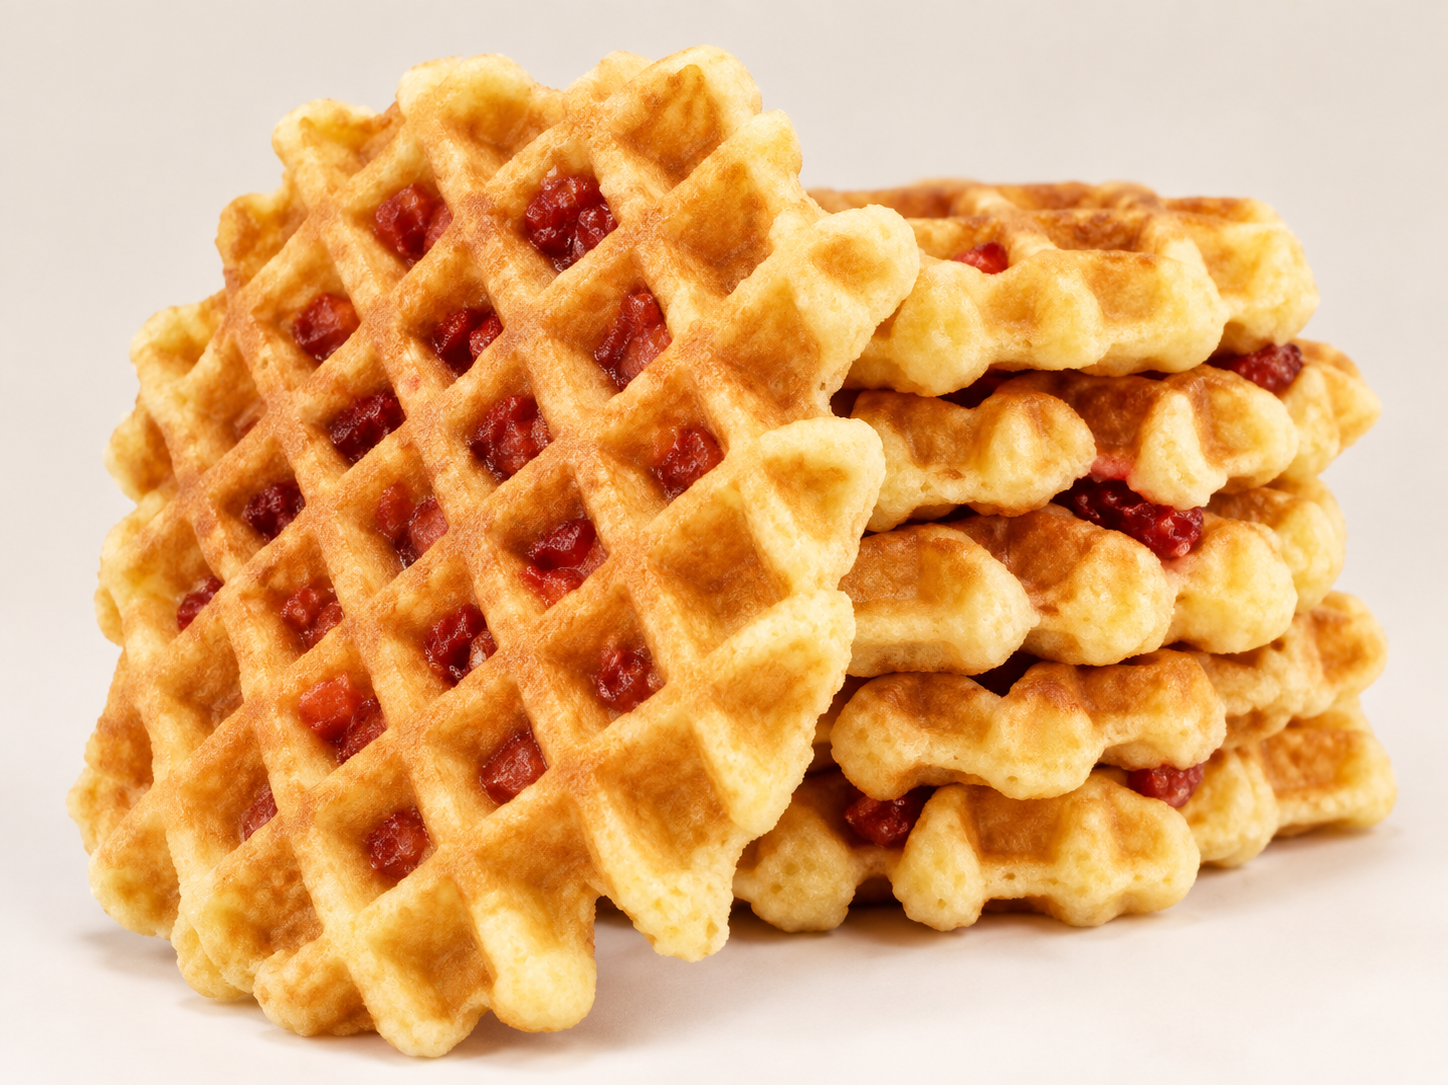
Variables That Define an Automation Project
Equipment choice can never be cavalier when cleanability, access, disassembly, inspection, and maintenance remain undefined. That gap creates integration and food-safety risk because FDA hazard-analysis inputs, utilities and line interfaces must be reviewed alongside the product target. UD Company uses these inputs to frame the equipment specification before the project scope is decided.
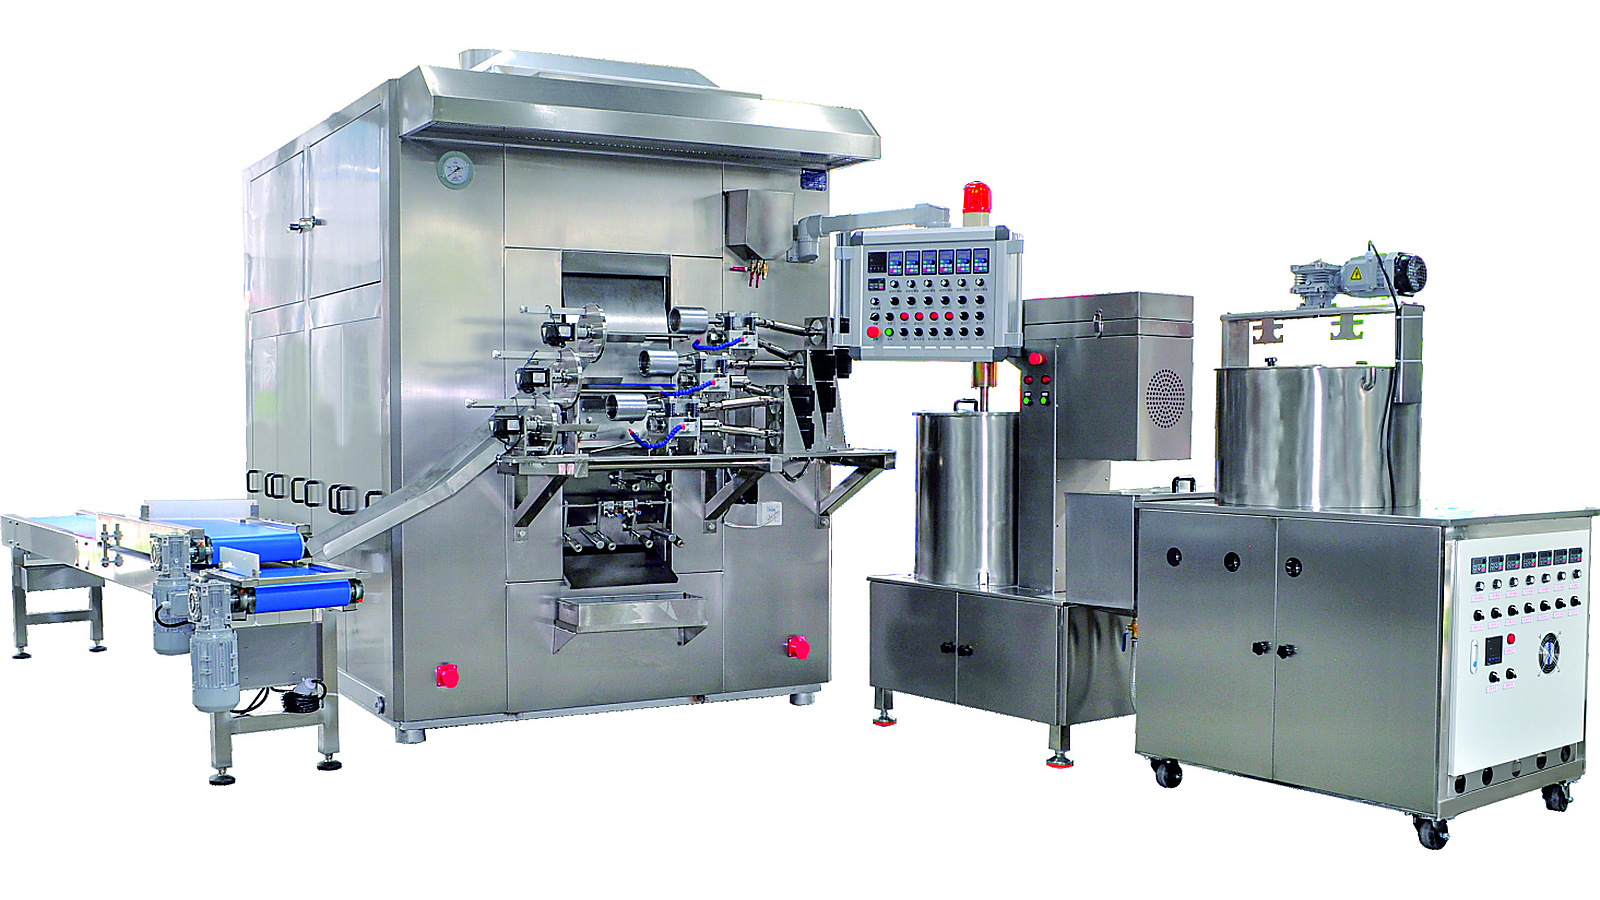
Formula and inputs
Record what can vary before the bake
- Formula revision and ingredient percentages by weight
- Flour type, protein content and lot identity
- Sugar, fat, egg, water, salt and leaven system
- Mixing sequence, batter or dough temperature, and hold time
Product target
Define an accepted sample in measurable terms
- Piece geometry, mass and thickness
- Surface colour and browning distribution
- Crisp, chewy or tender texture target
- Moisture, cooling, packaging and intended shelf life
Food safety and hygiene
Bring hazard and cleaning inputs into the brief
- Ingredient and allergen profile
- Sanitation method and cleaning frequency
- Access, disassembly and inspection expectations
- Packaging, storage, distribution and intended use
These relate to the factor groups in 21 CFR 117.130 and bakery hygienic design guidance.23
Utilities and interfaces
Map the plant around the proposed machine
- Available power, fuel, water, air and exhaust
- Heating and cooling method
- Floor space, access and environmental conditions
- Upstream preparation and downstream packaging interfaces
Recent food-manufacturing energy guidance places process heat, steam, water heating, heat recovery, cooling, and packaging within one facility-level decision.4
Production plan
State the basis of capacity
- Product units or mass per hour
- Shift pattern and planned run length
- SKU count and changeover sequence
- Operator, quality and maintenance responsibilities
Acceptance evidence
Agree on what closes the trial
- Reference sample and formula version
- Measurement method and sample location
- Acceptable range for each output
- Deviation, retest and sign-off record
Choose the Right Evidence Path
The wrong answer is to provide one guide for both ingredient and outcome questions because they require different evidence. The ingredient path is composed of formula functions, and the outcome path is composed of moisture, browning and texture. The unresolved risk indicates where to look next: open the corresponding guide, then return to the equipment brief.
Baking Ingredients and Their Functions
Review flour function in baking, sugar function in baking, fat, egg and other functions of baking ingredients without turning this parent page into a detailed ingredient guide.
Open the ingredient guide
Baking Texture, Browning and Moisture
The texture guide includes baked-goods texture, moisture, finished color, crispness and Maillard reaction in baking examples as finished-product evidence.
Open the texture guideBuild an Operating Window, Not a Universal Setpoint
Unlike a generic baking temperature and time chart, a controlled operating window is tied to the formula, piece geometry, heating method and accepted result. The trade-off is timing: a team that checks texture only after the outcome is complete may find the problem after the batch can no longer be corrected. Variable incoming moisture has the potential to cause a finished product to be inconsistent, reworked, or dried and rejected if an acceptance specification is not checked at the appropriate time.
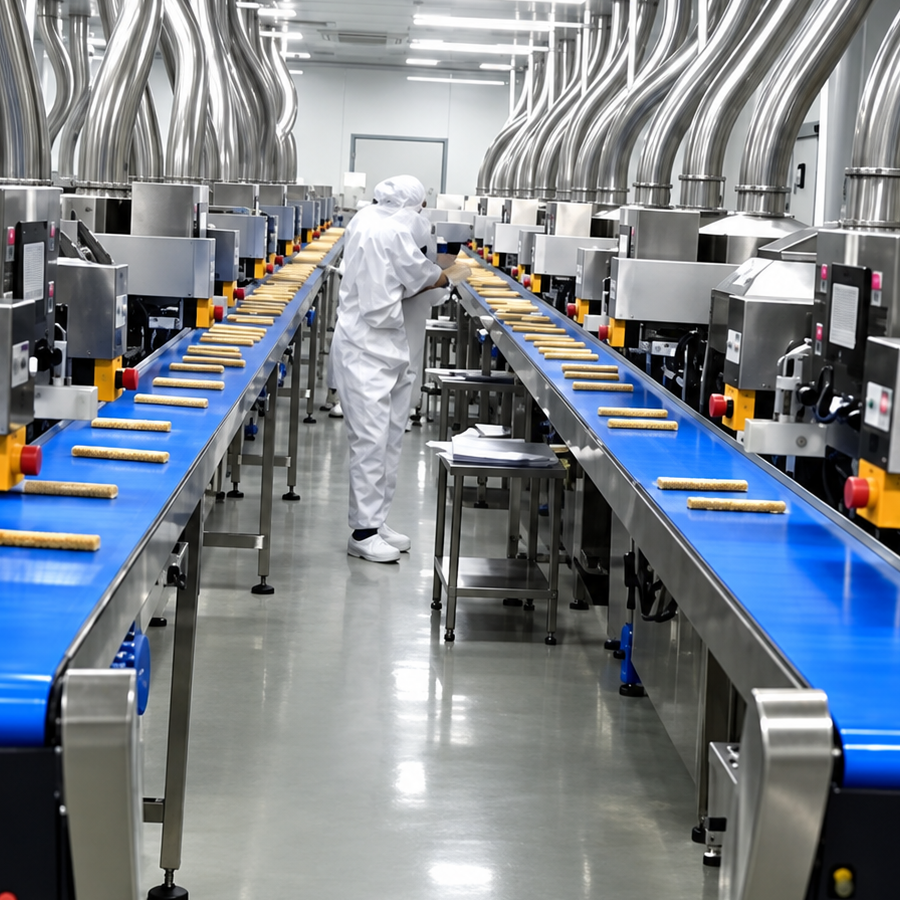
10-Field Operating Window Record
| Row | Field | Unit or format | Record during the trial | Acceptance owner |
|---|---|---|---|---|
| 01 | Formula identity | Revision + % by weight | Ingredient lot, sequence and any substitution | R&D / quality |
| 02 | Mixed mass condition | °C + elapsed min | Discharge temperature and hold time before depositing | Process / production |
| 03 | Deposit or portion | g per piece | Set value and sampled actual mass | Production / quality |
| 04 | Product geometry | mm | Thickness, diameter, length or roll form | R&D / quality |
| 05 | Heating condition | °C by contact surface or zone | Setpoint, observed value and measurement location | Process / maintenance |
| 06 | Bake or contact time | s or min | Cycle value and actual residence time | Process / production |
| 07 | Moisture result | % or water-activity method | Sample location, instrument, calibration and result | Quality |
| 08 | Colour result | L*a*b* or approved image standard | Top, bottom and edge distribution | Quality / R&D |
| 09 | Texture result | N, bend method or defined sensory scale | Test timing after cooling and observed result | R&D / quality |
| 10 | Defect result | % of a defined sample | Cracks, sticking, deformation, uneven brown areas and rejects | Production / quality |
Interaction-Aware Formulation and Process Validation
Scaled recipes may require changes to equipment, mixing time, temperature and bake time, in addition to ingredient quantities. One biscuit-model study demonstrated that changes to formulation and baking time combined to affect the structure, hardness, moisture, and non-enzymatic browning of the biscuit. The error is to change interrelated factors without a clear comparison; determine how the change affects the approved sample prior to adjusting the operating range.
Keep the approved sample, formula revision and measurement method together.
Check ingredient lot, mixed-mass condition, deposit and plant environment before changing the machine.
Use one-variable trials only where the expected interaction risk is low.
Change two linked factors deliberately when one factor may alter the effect of the other.
Repeat the selected condition across the relevant lot, shift or run boundary before acceptance.
The Evidence Escalation Sequence
NIST demonstrates that one-factor-at-a-time experiments can ignore interactions when the effect of one input is dependent upon another input setting. Therefore, the strategy progresses from a limited screen to paired factors only when the cause and effect map supports it.
| Formula variable | Linked process variable | Outcome to observe | Decision use |
|---|---|---|---|
| Sugar or reducing sugar | Surface temperature and time | Browning reaction, moisture loss and release | Separate colour development from over-drying |
| Flour protein and gluten potential | Mixing energy and hold time | Flow, gas retention and final structure | Distinguish formula response from depositing instability |
| Fat system | Cooling and release timing | Fragility, crispness and surface release | Find whether breakage begins at bake, release or cooling |
| Baking powder or baking soda | Mixed-mass hold time | Gas response, shape and cell structure | Check whether the leaven response changes before heating |
| Deposit mass | Bake or contact time | Centre moisture, edge colour and texture | Define a repeatable product geometry window |
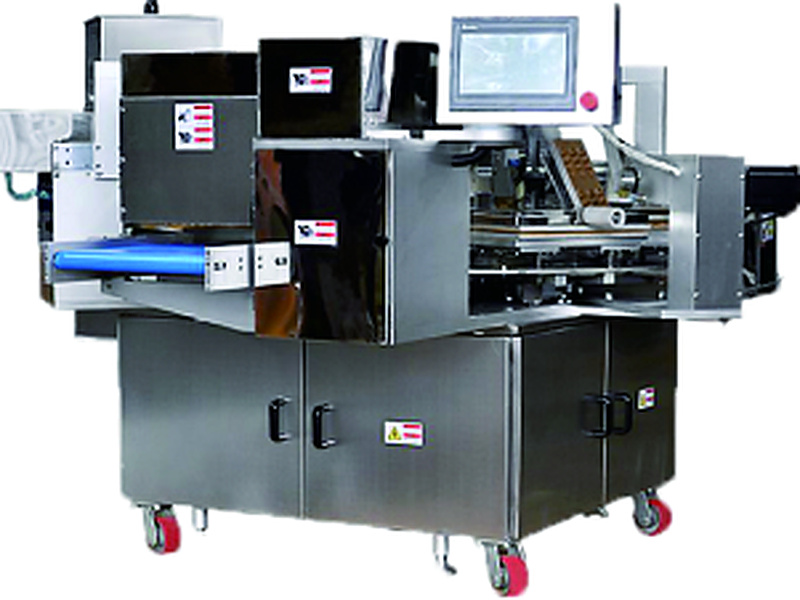
Project Cost, Lead Time and Commercial Terms
Purchase price can hide installation, commissioning, training, spares, software, downtime and retired-asset costs.5 The trade-off becomes visible only when every quotation uses the same project boundary and buyer baseline.
The 8-Layer Bakery Integration Cost Envelope
Layer
Cost field
Buyer input
Hidden bottleneck to check
01
Equipment
Quoted machine and included scope
Excluded auxiliary equipment
02
Installation
Freight, placement, utilities and site work
Facility readiness
03
Commissioning
Trial material, technician time and acceptance run
Undefined product criteria
04
Training
Operator, quality and maintenance time
Shift coverage
05
Spare parts
Opening stock and replenishment plan
Critical-part lead time
06
Lifecycle support
Maintenance, software and technical service
Responsibility boundary
07
Production interruption
Installation, changeover and unplanned downtime
Lost contribution during the stop
08
Retired assets
Removal, write-off or retained backup use
Double-counted capacity
How We Work: UD Company Food Automation Capability
UD Company automates the production of foods. The following descriptions define us; they are company facts, not substitutes for a product-specific sample.
-
At UD Company, we were established in 2003.
-
UD Company operates in the High-tech Development Zone of Xinyu City, Jiangxi Province.
-
Our investment at this operating base is nearly RMB 200 million.
-
The site covers 130 acres.
-
Our manufacturing footprint includes two major production bases.
-
Research and development focuses on food production automation technology.
-
We independently developed our fully automatic egg roll machine series.
-
We independently developed our fully automatic phoenix tail roll machine series.
-
Our equipment series hold multiple invention patents.
-
Our users span domestic and international markets.
How We Work: From Product Target to Technical Review
A useful inquiry begins with a specific baked product rather than a cataloged machine model. The brief will assist in determining if the question pertains to the development of the formula, the validation of the process, the configuration of the machine, or the integration of the plant.
Share the target
Send the product type, geometry, approved sample and market.
Define the basis
State formula version, batch context, desired output and changeover plan.
Map the plant
Confirm space, utilities, sanitation and line interfaces.
Plan the evidence
Agree on measurements, trial sequence and acceptance result.
Set the scope
Receive the proposed configuration, included items and commercial terms.
Engineering Planning & Calculation Tools
Frequently Asked Questions
What is baking science in industrial production?
Overview
Baking science connects formula, preparation, heat and moisture movement to product structure and measurable finished-product quality.
Is baking simply chemistry?
Dynamics
Chemical reactions matter, including gas generation and the Maillard reaction, but physics and operations matter too. Heat transfer, water movement, geometry, contact, cooling and line timing help determine whether a baked product reaches its target.
Can a baking temperature and time chart define a production setting?
Variables
No single chart can account for formula, piece mass, heating method, contact area, moisture target and cooling. Treat a chart as a starting hypothesis, then confirm an operating window against the approved product.
Why do familiar products respond differently?
Structure
A chocolate chip cookie dough, a cream pastry and an egg-roll batter do not share the same structure or process path. The same science behind baking applies, but each product needs its own formula, measurement method and acceptance record.
Which ingredient questions belong in the detailed guide?
Scope
Use the ingredient guide for bread flour, cake flour, starch, sugar, fat, egg, baking soda, baking powder and the function of leavening agents in baking. This page keeps only the causal overview needed for an industrial project decision.
How does UD Company start a project review?
Process
Share the product target, formula context, piece geometry, desired output, utilities, sanitation needs and packaging interface. The technical team separates formula questions from machine configuration, plant integration and food-safety responsibilities, then identifies the measurements that must travel with the trial. The resulting review scope can cover interfaces, operating-window evidence, quotation inclusions, lead time, payment method and the acceptance path without turning an early estimate into a performance guarantee.